How to Prevent Tool Chatter in CNC Machining (Causes and Fixes)
Chatter has been frustrating machinists since before CNC existed. As early as 1907, Frederick W. Taylor described machining vibrations as the most obscure and delicate of all the problems facing the machinist — and that observation still holds up, as shown in the many publications on machining that followed.
This guide explains what chatter actually is, why it happens, and the specific, evidence-based fixes that reduce it — rather than the trial-and-error approach that’s still how most setups get tuned in practice.
Fighting chatter on a specific job? Tell our team the setup — tool overhang, workpiece, and operation — and we’ll help you troubleshoot it.
What Chatter Actually Is
In machining, vibrations — also called chatter — are the relative movements between the workpiece and the cutting tool. These vibrations can range from quiet and barely noticeable to very violent, and they result in wave patterns left on the machined surface. The problem affects typical machining processes such as turning, milling, and drilling, and even atypical processes like grinding, where a wheel that’s out of true leaves an irregular surface flaw known as a chatter mark.
The key breakthrough in understanding chatter came in 1958, when S. A. Tobias and W. Fishwick explained machine tool regenerative chatter by modelling the feedback loop between the metal cutting process and the machine tool structure — work that produced the stability lobes diagram still used today. Three parameters define the limit where machining vibration is prone to grow over time: structure stiffness, damping ratio, and the machining process damping factor.
Two Types of Vibration: Forced and Self-Generated
Vibration problems generally result in noise, poor surface quality, and sometimes tool breakage. The main sources fall into two categories:
- Forced vibrations — mainly generated by interrupted cutting (inherent to milling), tool or workpiece runout, or vibrations transmitted from outside the machine.
- Self-generated vibrations (regenerative chatter) — related to the fact that actual chip thickness also depends on the relative position between tool and workpiece during the previous tooth passage. This creates a feedback loop: the current cut removes a wavy surface left by the previous cut, and that wave can grow larger with each pass, seriously degrading the machined surface quality.
Why High-Speed Machining Makes Chatter More Likely
High-speed machining (HSM) has enabled real productivity gains and made previously impossible workpieces — such as thin-walled parts — practical to produce. The trade-off is that machining centres running at these very high dynamic movements are inherently less rigid. In many applications, particularly long tools and thin workpieces, the appearance of vibration becomes the single most limiting factor, forcing the machinist to reduce cutting speeds and feeds well below what the machine or tool is actually capable of.

The Basic Rules for Avoiding Vibration
Mathematical models can simulate machining vibration quite accurately, but in practice it’s always difficult to avoid it entirely. There are four basic rules a machinist can apply:
- Make the workpiece, the tool, and the machine as rigid as possible.
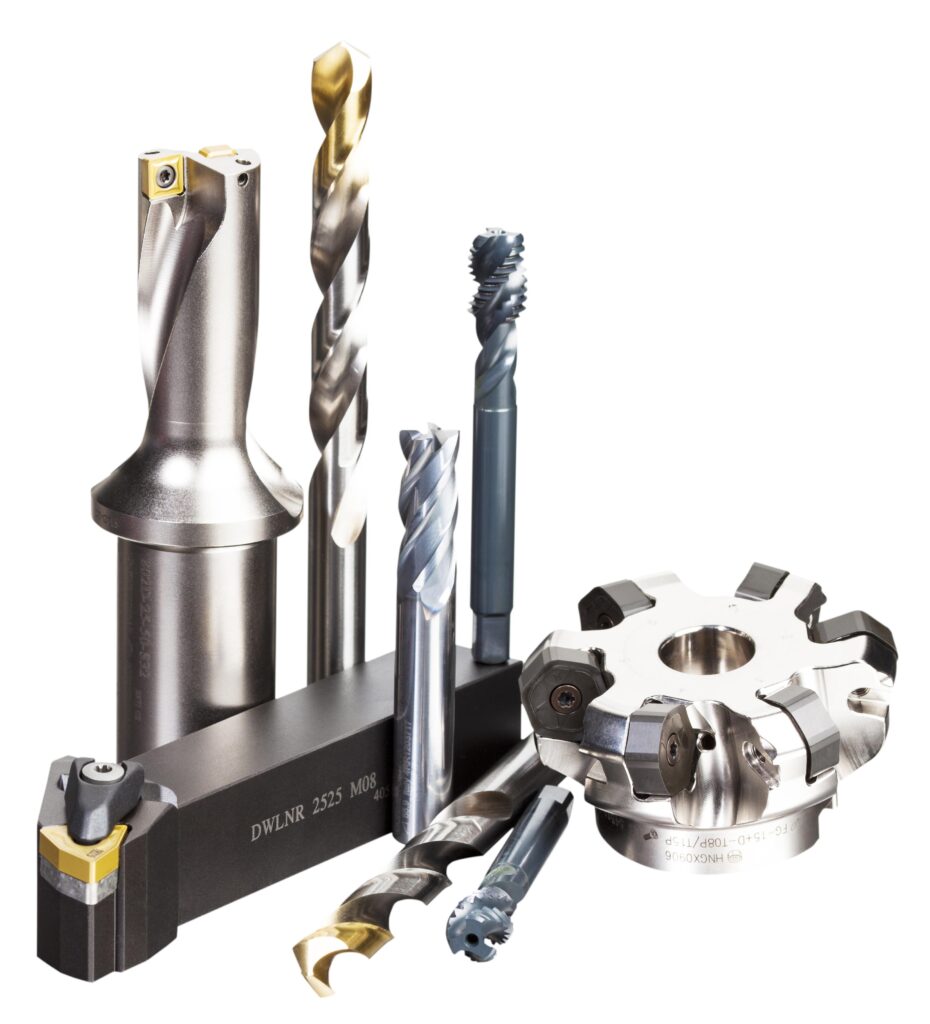
- Choose the tool that will least excite vibrations — modifying angles, dimensions, surface treatment, and so on.
- Choose exciting frequencies that best limit the vibrations of the machining system — spindle speed, number of teeth, and their relative positions.
- Choose tools that incorporate vibration-damping technology — structure damping using high-damping material in the joint areas, and mass dampers using a counteracting force to stabilize the motion.
Specific strategies have also been developed for thin-walled workpieces specifically — alternating small machining passes to avoid static and dynamic flexion of the walls, and reducing the length of cutting edge in contact with the workpiece to limit self-generated vibration.
Need a more rigid tool holder or damped tooling setup? Send us your tool overhang and operation and we’ll help you find the right equipment.
Tool Holder Rigidity and the L/D Ratio
Machining vibration often comes from the tool holder having a high length-to-diameter (L/D) ratio combined with low stiffness. Stiffening the tool holder with tungsten carbide material is a widely used fix when the tool diameter or weight is small, since tungsten carbide’s material cost isn’t prohibitive at that scale.
At a longer reach — an L/D ratio above roughly 4, up to around 14 — stiffening alone usually isn’t enough, and a mass damper becomes necessary to effectively damp out the vibration through a counteracting force on the tool structure. The simplest form of mass damper uses a heavy weight (made of tungsten or lead) supported by rubber rings, with or without a tuning mechanism; a tuning mechanism lets the damper cover a wider range of L/D ratios (which corresponds to a wider range of vibration frequencies). More advanced mass dampers use viscous fluid or damping oil to improve damping efficiency at the targeted frequency, and the latest designs use special polymers with frequency-dependent stiffness, allowing the damper to self-tune across a wider L/D range.
Hydraulic expansion tool holders also minimise vibration to a large extent, largely through precise control of total indicator reading (TIR) to less than 3 micrometres — this helps reduce vibration caused by an unbalanced load on the cutting edges, and what little vibration is still generated is largely absorbed by the oil inside the holder’s internal chambers.
Other Proven Fixes
Variable Tool Pitch
Beyond stability lobe theory, the use of tools with variable pitch between cutting edges often gives good results at a relatively low cost, and tool manufacturers increasingly offer these — though it does mean the shop can’t rely on a single standard tool across every job in the same way.
Spindle Speed Selection via Stability Lobes
Multiplying the models based on stability lobe theory makes it possible to find the best spindle speed for a given machining setup, producing robust predictions across different kinds of machining. In practice, this means choosing exciting frequencies (spindle speed, tooth count, tooth spacing) deliberately, rather than defaulting to whatever speed is most convenient.
Reducing the Length of Engaged Cutting Edge
Since self-generated vibration is tied to how much cutting edge is in contact with the workpiece, reducing that engaged length is a direct way to limit the feedback loop that drives regenerative chatter — this is part of why thin-wall strategies favour smaller, more frequent passes.
Matching the Fix to Your Situation
Long Tool Overhang
For a small-diameter tool with significant reach, a tungsten carbide shank addresses low L/D-ratio stiffness directly. Past an L/D ratio of roughly 4, a mass damper becomes the more appropriate solution, since stiffening alone can’t fully compensate at that reach.
Thin-Walled Workpieces
Alternating small machining passes and reducing the engaged length of cutting edge are the specific strategies developed for this case, rather than general-purpose tool stiffening alone.
Interrupted Cuts in Milling
Since forced vibration is inherent to milling’s interrupted cutting action, variable tool pitch and careful spindle speed selection (via stability lobes) are the more relevant tools here, alongside general rigidity.
High-Speed Operations on Less Rigid Machines
Where HSM’s reduced rigidity is the limiting factor, damping technology — mass dampers or hydraulic expansion holders — addresses the problem without simply backing off speed and feed below the machine’s real capability.
Common Mistakes When Troubleshooting Chatter
Assuming One Fix Covers Every Cause
Forced vibration (from interrupted cuts, runout, or outside sources) and self-generated regenerative chatter have different root causes, and the same fix won’t necessarily address both.
Defaulting to a Lower Spindle Speed as the Only Lever
Reducing speed and feed is the common fallback, but it sacrifices the productivity HSM was meant to deliver. Stability lobe-based spindle speed selection, variable pitch tooling, and holder stiffening or damping are all alternatives worth trying before settling for reduced throughput.
Ignoring the Tool Holder’s L/D Ratio
Chatter is frequently blamed on the insert or the cutting parameters when the actual source is a tool holder with a high L/D ratio and low stiffness — a problem that’s fixed at the holder, not the insert.
Skipping Small-Pass Strategies on Thin Walls
Treating a thin-walled part like a standard rigid workpiece, rather than alternating smaller passes, invites exactly the static and dynamic flexion these specific strategies were developed to avoid.
Sourcing Rigid Tooling for CNC Machining in Dubai
Khokhawala Trading LLC supplies premium carbide tooling systems for CNC machining, metal cutting, milling, turning, and drilling in Dubai and across the UAE.
KTRDG’s carbide tooling range includes products from Sandvik Coromant, Kennametal, Korloy, and Mitsubishi.
With more than 35 years of industrial tool supply experience, Khokhawala Trading LLC serves manufacturers, CNC shops, fabrication companies, and engineering industries in the UAE.
Ready to shop carbide tooling? Browse our carbide tooling systems range or reach out with your requirement for a fast quote.
A Quick Chatter Troubleshooting Checklist
- Is the vibration forced (interrupted cutting, runout, external source) or self-generated (regenerative chatter from the previous pass)?
- What is the tool holder’s L/D ratio, and does it need stiffening or a mass damper?
- Have you tried a stability lobe-informed spindle speed change before defaulting to a slower feed?
- Is the tool choice (angles, dimensions, surface treatment, variable pitch) contributing to the vibration?
- For thin-walled parts, are small, alternating passes being used rather than one deep pass?
- Is the length of engaged cutting edge minimised where self-generated vibration is the issue?
- Would a hydraulic expansion tool holder’s TIR precision help this specific setup?
Conclusion
Chatter comes from two distinct sources — forced vibration from interrupted cuts, runout, or outside disturbances, and self-generated regenerative chatter from the feedback loop between consecutive cutting passes — and effective fixes differ depending on which one is driving the problem. Rigidity, deliberate tool selection, informed spindle speed choice, and damping technology (mass dampers or hydraulic expansion holders) are the evidence-based levers, rather than simply backing off speed and feed and accepting lower productivity.
For businesses sourcing rigid, high-quality carbide tooling in Dubai, Khokhawala Trading LLC supplies Sandvik Coromant, Kennametal, Korloy, and Mitsubishi tooling for CNC machining, milling, turning, and drilling applications.
Still Fighting Chatter on a Job?
Send us your setup — tool overhang, workpiece, and operation — and Khokhawala Trading LLC will help you find the right tooling.
Tool Chatter in CNC Machining, Answered
Chatter is the relative movement between the workpiece and the cutting tool during machining. It ranges from barely noticeable to very violent, and it leaves wave patterns on the machined surface.
Forced vibration comes from interrupted cutting, tool or workpiece runout, or vibration from outside the machine. Self-generated (regenerative) vibration comes from the chip thickness depending on the tool-workpiece position left by the previous pass, creating a feedback loop that can grow over time.
Make the workpiece, tool, and machine as rigid as possible; choose a tool least likely to excite vibration; choose spindle speed and tooth configuration to limit excitation; and use tools with vibration-damping technology such as structure damping or mass dampers.
High-speed machining centres are less rigid because of the very high dynamic movements involved. In applications with long tools or thin workpieces, vibration often becomes the limiting factor, forcing reduced cutting speeds and feeds well below the machine’s actual capability.
Machining vibration often comes from a tool holder with a high length-to-diameter (L/D) ratio and low stiffness. Tungsten carbide stiffening helps for small-diameter tools, while an L/D ratio above about 4 generally needs a mass damper to effectively control the vibration.
A mass damper uses a counteracting force to stabilize tool motion. Simple versions use a tungsten or lead weight supported by rubber rings; more advanced versions use viscous fluid or frequency-dependent polymers to improve damping efficiency across a wider range of L/D ratios.
Yes. Hydraulic expansion tool holders minimise vibration largely through precise control of total indicator reading to less than 3 micrometres, reducing vibration from unbalanced cutting-edge load, with remaining vibration largely absorbed by the oil inside the holder’s internal chambers.
Stability lobe theory, developed from Tobias and Fishwick’s 1958 regenerative chatter model, helps find the best spindle speed for a given machining setup, allowing deliberate selection of exciting frequencies rather than relying on trial and error.
Alternating small machining passes, rather than one deep pass, helps avoid static and dynamic flexion of thin walls. Reducing the length of cutting edge engaged with the workpiece also limits self-generated vibration.
Khokhawala Trading LLC supplies carbide tooling systems in Dubai and across the UAE, including Sandvik Coromant, Kennametal, Korloy, and Mitsubishi products.